Precision Wire EDM Machining
Wire EDM for Difficult Alloys
AXALLOY Precision is a Shenzhen-based precision machining partner supporting international engineering, procurement, and quality teams with Wire EDM services for difficult-to-machine alloys. We specialize in complex, high-value components that demand tight tolerances, stable process control, and complete inspection documentation—from prototype validation to repeat production.
If you're machining materials like Inconel, Hastelloy, titanium, duplex stainless, or cobalt alloys, Wire EDM can be the most reliable way to achieve sharp internal corners, narrow slots, and distortion-sensitive profiles without introducing cutting forces.
Why Wire EDM for Difficult Alloys?
Difficult alloys are often selected for high-temperature strength, corrosion resistance, and fatigue performance—but those same properties can make conventional machining slow, tool-intensive, and risk-prone. Wire EDM is often the preferred process when you need:
- Minimal mechanical stress on thin walls or delicate features
- Consistent accuracy in hardened or tough conductive alloys
- Sharp internal geometry that is hard to mill (small corner radii, narrow slots)
- Stable repeatability for production runs with controlled output
AXALLOY's approach includes early review of material behavior, geometry, tolerances, surface requirements, inspection strategy, and production volume before defining the EDM route.
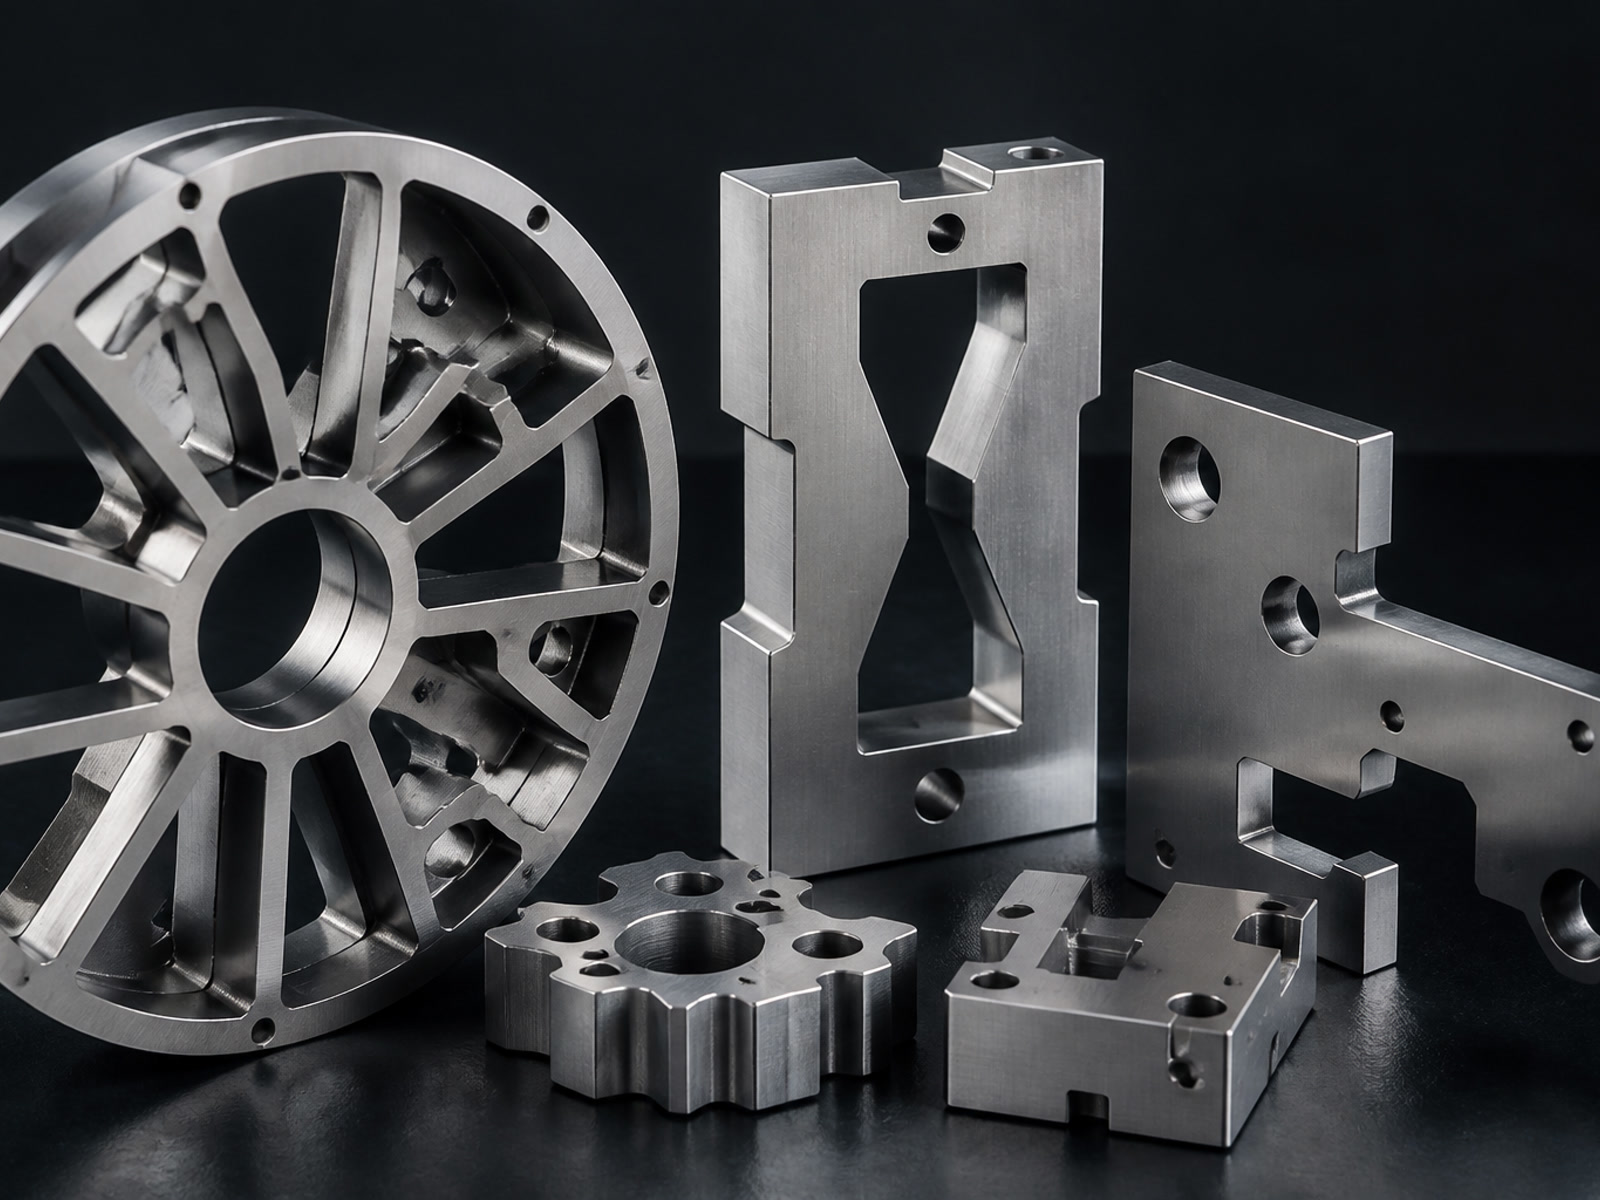
AXALLOY Wire EDM Capability (Standard)
Our Wire EDM capacity covers a broad range of workpiece sizes and precision requirements for difficult alloys.
Wire EDM Capacity & Performance
- Max workpiece size
- 600 × 400 × 300 mm
- Max workpiece weight
- 500 kg
- Wire diameter
- Ø0.10–0.30 mm
- Minimum cutting width
- 0.15 mm
- Cutting accuracy
- down to ±0.005 mm
- Repeatability
- ±0.003 mm
- Max cutting taper
- ±30°
- Surface finish
- down to Ra 0.8 μm
- Max cutting thickness
- 300 mm
Suitable EDM Features
- Narrow slots and thin webs
- Sharp internal corners
- Profiles and contours
- Precision inserts, punches, and die features
- Tight-fit interfaces requiring reliable feature relationships
Materials We Commonly Wire EDM (Difficult Alloys)
We routinely support Wire EDM for conductive difficult alloys including:
Nickel-Based Alloys
Inconel 625/718 and other Inconel series, Hastelloy C-22/C-276, Monel 400/K-500, Haynes alloys, Waspaloy/Nimonic/Rene families
Titanium Alloys
Grades 2/5/23 (note: Wire EDM requires conductivity and appropriate process planning)
Stainless Steels
316L, 17-4 PH, 15-5 PH, 420/440C and more
Duplex / Super Duplex
2205 / 2507
Cobalt-Based Alloys
Cobalt chrome, Stellite, L605, MP35N
Tool Steels / Hardened Steels
A2, D2, H13, M2
If you're unsure whether your specific grade is a fit for Wire EDM, send the material spec and drawing notes—our engineers will confirm feasibility and expected results.
Typical Wire EDM Applications (Best-Fit Projects)
AXALLOY is best suited to projects where manufacturability, documentation, and dependable communication matter as much as price. Wire EDM is frequently used in:
Aerospace: precision profiles, heat-resistant alloy features, controlled documentation packages
Medical devices: small, high-precision conductive components and tight feature control
Semiconductor equipment: precision slots, complex profiles, repeat build consistency
Energy / oil & gas / marine: corrosion-resistant alloy parts with traceability needs
Robotics & automation: precision interfaces and repeatable components for assemblies
Best-Fit Technical Profile
- Thin walls, critical interfaces, tight GD&T, demanding surfaces
- Difficult holes/slots where milling is high-risk or unstable
- Parts sensitive to distortion or requiring stable geometry relationships
Tolerance, Surface Finish & Secondary Processes
Wire EDM is often selected for accuracy and geometry, then paired with finishing processes to meet final requirements.
Secondary Finishing Options
- Precision grinding: down to ±0.002 mm, surface finish down to Ra 0.2 μm
- Deburring, cleaning, marking
- Heat treatment, passivation, coating (as specified)
Inspection, Traceability & Quality Documentation
For difficult-alloy EDM parts, quality evidence is often part of the deliverable. We support inspection planning and documentation suitable for international OEM and supplier requirements.
Inspection Capabilities
- CMM range
- 700 × 1,000 × 600 mm
- CMM accuracy
- up to 1.8 + L/300 μm
- Optical measurement
- ±0.002 mm
- Surface roughness
- Ra 0.05–40 μm
- Hardness testing
- Rockwell / Brinell / Vickers
Temperature-controlled inspection room; calibrated equipment
Documentation Available (Project-Specific)
- Material Test Report / Mill Test Certificate
- Certificate of Conformance (CoC)
- First Article Inspection (FAI) + ballooned drawing
- Full dimensional reports, surface roughness report
- Heat treatment / coating certificates (when applicable)
- Material and lot traceability; special process records
- Inspection photos upon request
Prototype to Repeat Production Support
We support Wire EDM projects from 1 part prototypes to repeat low-volume and batch production.
5–10 days
Prototype lead time (typical)
10–20 days
Standard lead time
1–10,000+
Supported production volume (parts)
1 part
Minimum order quantity
Expedited service: available
File Formats We Accept
To quote accurately and reduce iteration time, we recommend sending both 3D and 2D.
3D Formats
STEP/STP, IGES/IGS, X_T, X_B, SLDPRT, SAT
2D Formats
PDF, DWG, DXF
What to Include in Your RFQ
To match your expectations for tolerance, finish, and documentation, include:
- 1 2D drawing + 3D model (preferred)
- 2 Material grade and condition (e.g., Inconel 718, solution treated/aged if applicable)
- 3 Quantity and expected repeat demand
- 4 Critical features, GD&T callouts, and inspection requirements
- 5 Surface finish requirements (EDM finish vs. post-finish)
- 6 Target delivery date and any packaging/export requirements
We'll respond with manufacturability feedback (DFM), process route, inspection approach, and a quote aligned with your risk and quality needs.
Request a Wire EDM Quote for Difficult Alloys
If your project involves tight-tolerance profiles, narrow slots, sharp corners, or distortion-sensitive features in difficult alloys, AXALLOY Precision can support a controlled, repeatable Wire EDM process with the documentation your engineering and quality teams expect.
Send your drawings and requirements to receive:
- Feasibility review + DFM notes
- Recommended EDM parameters/approach (based on geometry/material)
- Quote with lead time and quality deliverables
Request a Quote
Tell us about your component requirements and material challenges.