Difficult-Alloy Precision CNC Machining
Small Precision Turned Parts for Difficult Alloys
We produce small precision turned parts with tight, stable tolerances in nickel-based superalloys, titanium, PH stainless steels, duplex grades and cobalt alloys. From prototypes to repeat production, we help engineering, procurement and quality teams reduce risk, validate design intent earlier and receive the documentation needed for regulated markets.
AXALLOY is based in Shenzhen and works with customers in aerospace, medical devices, semiconductor equipment, energy, oil and gas, marine, robotics and advanced industrial equipment.
What you get when you work with us
Reliable dimensional control on small, critical features
Repeatable tolerances down to ±0.005 mm and roundness down to 0.005 mm help your assemblies fit and seal the first time.
Stable processes for difficult-to-machine alloys
We tune cutting parameters, tooling, coolant and fixturing for Inconel, Hastelloy, titanium and PH stainless steels so you don't lose time to trial-and-error at another shop.
Faster path to design validation and release
Prototype lead times of 5–10 business days let you test functional interfaces earlier, lock tolerances with evidence and keep program milestones on track.
Documented quality for regulated markets
Material certification, first article inspection and full dimensional reports reduce audit friction and simplify incoming inspection.
Clear communication and controlled change
You get DFM feedback up front, a defined production route and transparent updates so there are no surprises when parts arrive.
Best-fit projects
- Complex geometry with thin walls, critical runout or demanding surfaces
- Small precision turned parts in challenging alloys (Inconel 718/625, Hastelloy C-276/C-22, 17-4 PH, 15-5 PH, Titanium Grade 5/23, MP35N)
- High-value prototypes, low-volume or high-mix production, repeat programs
- Parts requiring material traceability, FAI/FAIR and project-specific records
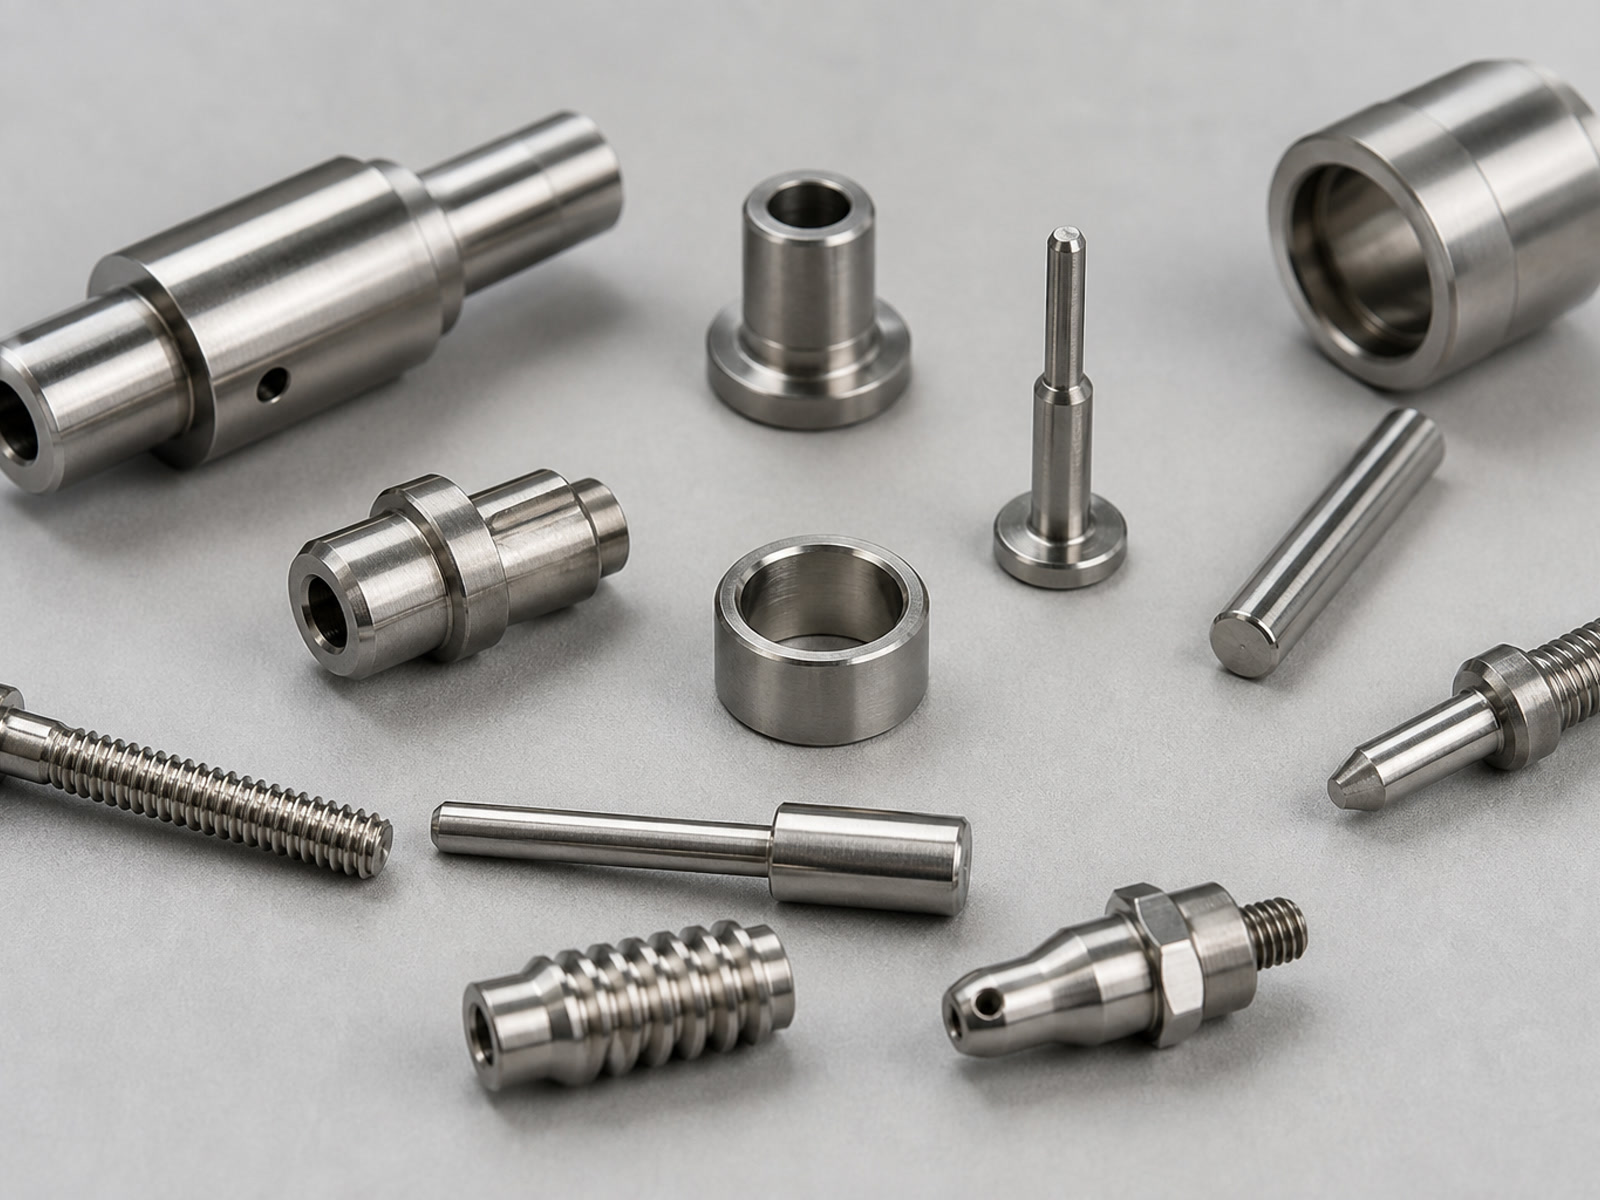
Typical small precision turned parts we deliver
- Micro and small shafts, pins and axles with tight runout
- Threaded fittings and connectors with controlled seal surfaces
- Nozzles and orifices with small, concentric bores
- Medical and instrumentation fasteners in titanium and MP35N
- Valve components and mini body seats in duplex and Inconel
- High-strength fasteners and bushings in 17-4 PH and 15-5 PH
Capabilities at a glance
Three complementary turning platforms cover your small precision turned parts from micro components to larger rotational parts.
Swiss CNC Turning
| Maximum bar diameter | Ø32 mm |
| Minimum part diameter | Ø0.5 mm |
| Maximum part length | 300 mm |
| Controlled axes | Up to 7 |
| Maximum spindle speed | 10,000 rpm |
| Turning tolerance | Down to ±0.005 mm |
| Repeatability | ±0.003 mm |
| Minimum thread size | M0.8 |
| Supported operations | Turning, milling, cross drilling, slotting, threading, back working |
| Typical parts | Small shafts, pins, screws, connectors, medical components, precision fittings |
Precision CNC Turning
| Maximum turning diameter | Ø500 mm |
| Maximum turning length | 1,000 mm |
| Maximum bar capacity | Ø80 mm |
| Maximum spindle speed | 5,000 rpm |
| Chuck size | 6–15 inches |
| Turning tolerance | Down to ±0.005 mm |
| Diameter tolerance | Down to ±0.005 mm |
| Concentricity | Down to 0.008 mm |
| Roundness | Down to 0.005 mm |
| Minimum machined diameter | Ø1.0 mm |
| Minimum thread size | M1.0 |
| Supported operations | Turning, facing, grooving, threading, boring, drilling, parting |
Mill-Turn
Complex multi-feature parts in one setup
| Configuration | Main spindle, sub-spindle, C-axis, Y-axis, live tooling |
| Maximum machining diameter | Ø400 mm |
| Maximum machining length | 800 mm |
| Maximum bar capacity | Ø65 mm |
| Maximum spindle speed | 6,000 rpm |
| Live-tool speed | Up to 12,000 rpm |
| Controlled axes | Up to 9 |
| Typical tolerance | ±0.008 mm |
| Supported operations | Turning, milling, drilling, tapping, boring, grooving, off-center features |
| Typical parts | Complex shafts, valve bodies, connectors, nozzles, multi-feature rotational components |
Surface finish and secondary operations
Materials we machine for small turned parts
Nickel-based alloys
Inconel 718/625/600/601/690/706/725, Hastelloy C-276/C-22/B-2/X, Monel 400/K-500, Haynes 188/230/282, Waspaloy, Nimonic
Titanium
Grade 2, Grade 5 (Ti-6Al-4V), Grade 9, Grade 12, Grade 23 (ELI)
Stainless steels
17-4 PH, 15-5 PH, 316L, 304, 321, 410, 420, 440C
Duplex and super duplex
2205, 2507
Cobalt alloys
Stellite, L605, MP35N, CoCr
High-temp steels
A286, Nitronic 50/60
Specialty metals
Nitinol, molybdenum, tungsten, copper-nickel alloys
We evaluate material behavior, geometry, tolerances, surfaces, inspection strategy and volume before locking the machining process. This upfront work reduces scrap, stabilizes cycle time and yields consistent results lot after lot.
Inspection and documentation
| CMM measuring range | 700 × 1,000 × 600 mm |
| CMM accuracy | Up to 1.8 + L/300 μm |
| Optical measurement | ±0.002 mm |
| Surface roughness | Ra 0.05–40 μm |
| Thread inspection | Thread gauges and optical measurement |
| Environment | Temperature-controlled inspection room |
| Documentation | MTR/MTC, CoC, FAI/FAIR, ballooned drawings, full dimensional reports, special process records, heat treatment and coating certs, traceability |
What this means for you
Incoming inspection is faster, audit evidence is ready, and nonconformances are prevented—not explained after the fact.
Lead times and how speed helps your program
- Prototype lead time: 5–10 business days
- Standard lead time: 10–20 business days
- Expedited service: available on request
- MOQ: 1 part, volumes from 1 to 10,000+ pieces
Faster prototypes let you validate critical fits and threads earlier, freeze tolerances with measurement evidence, and align supplier capacity with your ramp plan. Short, reliable lead times reduce buffer stock and help procurement hit delivery targets without inflating inventory.
How we keep small turned parts consistent
Material control
Lot-traceable bar stock, verified hardness and condition to ensure predictable cutting performance.
Tooling and setup
Guide bushing and collet selection matched to diameter; tool stick-out minimized to control chatter on small diameters.
Cutting data by alloy family
Conservative entry parameters for nickel alloys; high-pressure coolant and chip control to prevent built-up edge.
In-process inspection
SPC on critical dimensions, thread gauges at defined intervals, and go/no-go controls for key fits.
Deburr and clean
Controlled deburring to protect edges and threads; cleaning and passivation where required by spec.
Documentation discipline
FAI on first lot, recorded process parameters and inspection plans support repeatability.
DFM tips for small precision turned parts
Send us your drawing early—we'll review for manufacturability and propose practical changes that protect function and schedule.
Tolerances
Assign tight tolerances only to functional features; we can hold ±0.005 mm where needed, but relaxing non-critical dimensions improves repeatability and cost.
Runout and concentricity
Call out datum structure; specify runout at the assembly-critical diameter rather than across multiple features.
Threads
Include thread reliefs where possible; specify class/fit and surface finish on sealing threads; note any thread locking compound needs.
Thin walls
For walls under 0.5 mm, flag as critical; we may suggest minor geometry changes or a different route (e.g., grind or EDM) for stability.
Cross holes
Provide exact positional requirements and deburr criteria; we can machine and deburr cross ports, but access and edge conditions should be defined.
Surface finishes
State Ra and inspection location; a default Ra 1.6 μm is suitable for most features, while sealing faces may need Ra 0.4–0.8 μm or grinding.
RFQ checklist
Include the following so we can quote quickly and accurately:
- 2D drawing (PDF) with dimensions, tolerances, material, heat treatment, finish and critical features
- 3D model (STEP/IGES) for geometry reference
- Quantity by lot and total annual volume
- Required documentation (e.g., MTR, FAI, full dimensional report, special-process certs)
- Target delivery date and any milestones
- Packaging, cleanliness and labeling requirements
- Any prior issues or special risks to watch
Supported file formats
| 3D CAD | STEP, STP, IGES, IGS, X_T, X_B, SLDPRT, SAT |
| 2D drawings | PDF, DWG, DXF |
| Images | JPG, PNG, TIFF |
| Compressed | ZIP, RAR |
| Units | Millimeters or inches |
| Max upload | 500 MB per RFQ |
How to start
Email your RFQ with drawings and models.
We perform a DFM and process review, then issue a detailed quote with any risk notes.
On order, we lock the process plan and inspection strategy.
You receive parts on the agreed schedule with the documentation you specified.
If you need immediate feasibility feedback on a small precision turned part in a difficult alloy, send your files and requirements—we'll respond with clear options, risks and lead-time scenarios so you can make a confident decision.
Get a Quote TodayRequest a quote for small precision turned parts
Send us your drawings and specifications. Our engineering team will review your project and respond with a detailed quote, DFM feedback, and lead time options.
info@alloycncmachining.com
Phone / WhatsApp
/
Address
Request a Quote
Tell us about your component requirements and material challenges.