RFQ-Ready Precision Machining
Tool Steel CNC Machining That Holds Size After Heat Treatment
When you need tool steel CNC machining for parts that must hold size after heat treatment, match a mating interface, or survive real production use, the focus is one thing: a controlled machining route that you can quote, approve, and repeat—with the inspection records to support it.
Supporting international engineering, procurement, and quality teams from prototype validation through low-volume and repeat production, especially when parts are complex or the previous supplier created schedule and quality risk.
What You Get When You Send an RFQ
1. A Machining Plan That Protects Your Tolerances
Early feedback on datums and stack-ups that drive true position, flatness, and concentricity; where tool steel may move after roughing/heat treat and how to control it; practical adjustments that reduce risk without changing function.
Outcome: Fewer drawing revisions, fewer nonconformances, and a production route that doesn't collapse when quantities increase.
2. Fewer Setups for Better Feature-to-Feature Relationships
For parts that mix rotational and prismatic features, mill-turn and multi-axis milling reduce re-clamping.
Outcome: Tighter relationships between critical features, more consistent repeat runs, and less variation between lots.
3. Documentation Ready for Audits
Material certification and traceability records, FAI and full dimensional reports, and special-process certificates when required.
Outcome: Faster supplier approval and fewer back-and-forth emails during PPAP/FAI-style reviews.
4. Fast Machining That Helps You Hit Program Milestones
Validate fit/function before committing to fixtures or large material buys; pull forward design verification and assembly trials; reduce downtime from unreliable suppliers.
Outcome: Less schedule risk and fewer costly late-stage design loops.
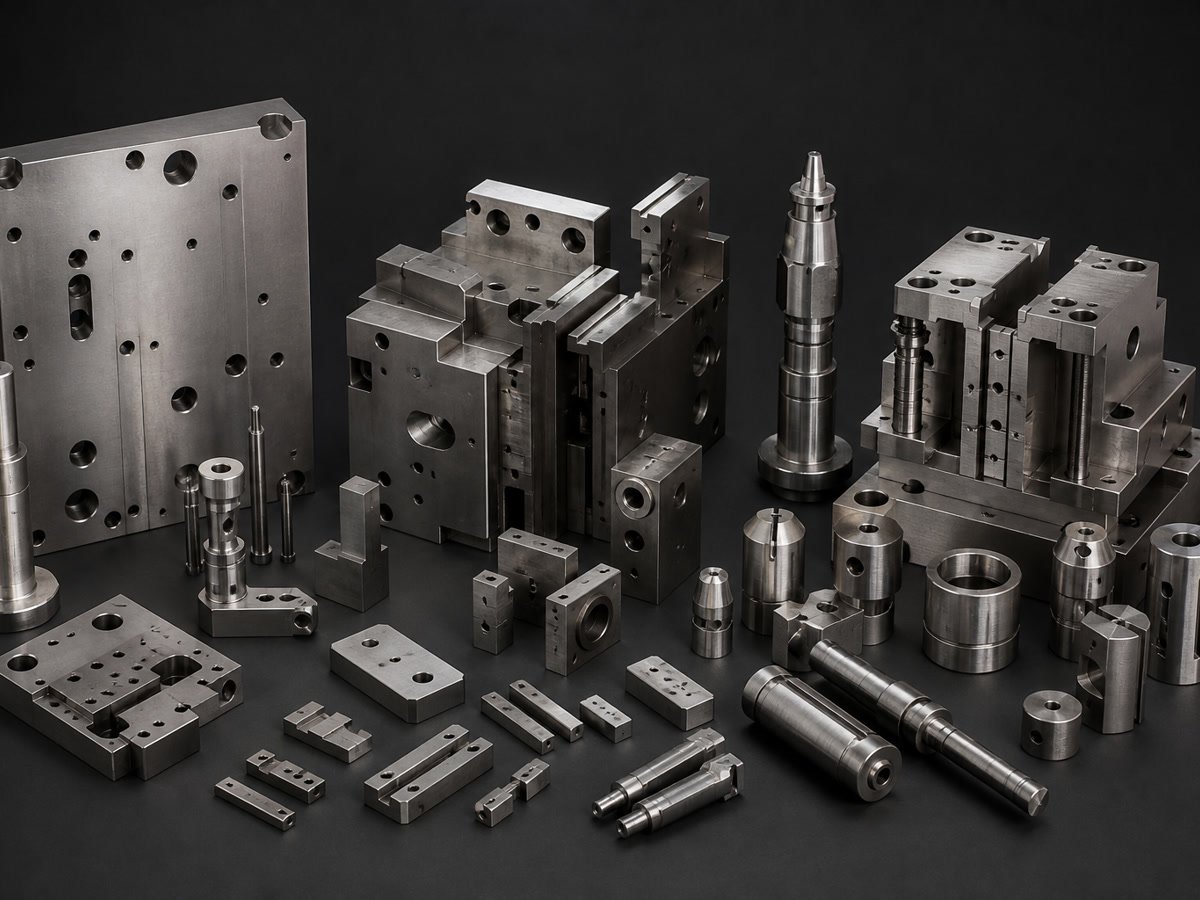
Tool Steel Parts Typically Machined
- Precision inserts, punches, dies, and wear components
- Hardened or semi-hardened fixtures, nests, and locating tooling
- Housings/plates with tight flatness, alignment bores, or dowel patterns
- Components requiring EDM sharp internal corners or narrow slots
Unsure whether your design is best milled, turned, ground, or EDM'd? Include your drawing/model in the RFQ—a stable route will be proposed.
Tool Steel Materials
| Material Group | Typical Grades |
|---|---|
| Tool Steels | A2, D2, H13, M2 |
If you have a specified hardness condition or heat treat standard, include it in the RFQ—machining strategy and inspection checkpoints often depend on it.
Capabilities Relevant to Tool Steel CNC Machining
Comprehensive machining, EDM, grinding, and inspection capabilities to support your most demanding tool steel components.
General Machining Capability
| Supported production volume | 1–10,000+ parts |
| Prototype quantity | 1–20 parts |
| Low-volume production | 20–500 parts |
| Batch production | 500–10,000+ parts |
| Standard dimensional tolerance | ±0.010 mm |
| Precision dimensional tolerance | ±0.005 mm |
| Position tolerance | Down to 0.010 mm |
| Flatness | Down to 0.005 mm |
| Concentricity | Down to 0.008 mm |
| Standard surface finish | Ra 1.6 μm |
| Precision machined finish | Ra 0.8 μm |
| Ground surface finish | Down to Ra 0.2 μm |
| Minimum wall thickness | 0.5 mm |
| Minimum machined hole diameter | Ø0.5 mm |
| Minimum thread size | M1.0 |
| Standard lead time | 10–20 business days |
| Prototype lead time | 5–10 business days |
| Expedited service | Available |
| MOQ | 1 part |
| Drawing units | Metric and Imperial |
CNC Milling
| Machining types | 3/4/5-axis CNC milling |
| Max 3-axis part size | 1,000 × 600 × 600 mm |
| Max spindle speed | 20,000 rpm |
| Positioning accuracy | ±0.005 mm |
| Repeatability | ±0.003 mm |
| Milling tolerance | Down to ±0.005 mm |
| Min internal corner radius | R0.3 mm |
| Supported operations | Facing, contouring, pocketing, drilling, tapping, boring, thread milling |
CNC Turning / Mill-Turn
| Turning tolerance | Down to ±0.005 mm |
| Max turning diameter / length | Ø500 mm / 1,000 mm |
| Mill-turn configuration | Main + sub-spindle, C/Y-axis, live tooling |
| Max mill-turn diameter / length | Ø400 mm / 800 mm |
| Controlled axes | Up to 9 axes |
| Typical mill-turn tolerance | ±0.008 mm |
EDM and Grinding
| Process | Capability Highlights |
|---|---|
| Wire EDM | Accuracy down to ±0.005 mm, surface finish down to Ra 0.8 μm, taper up to ±30° |
| Sinker EDM | Min internal corner radius R0.05 mm, surface finish down to Ra 0.4 μm |
| Precision grinding | Tolerance down to ±0.002 mm, flatness down to 0.003 mm, Ra down to 0.2 μm |
Inspection Capability
| CMM measuring range | 700 × 1,000 × 600 mm |
| CMM accuracy | Up to 1.8 + L/300 μm |
| Optical measurement accuracy | ±0.002 mm |
| Surface roughness range | Ra 0.05–40 μm |
| Hardness testing | Rockwell, Brinell, Vickers |
| Inspection environment | Temperature-controlled room |
| First article inspection | Available |
| Full dimensional inspection | Available |
Documentation Available
| Material Test Report / Mill Test Certificate | Available |
| Certificate of Conformance | Available |
| First Article Inspection Report | Available |
| Ballooned drawing + dimensional report | Available |
| Surface roughness report | Available |
| Heat treatment / coating certificate | Available |
| Material & lot traceability | Available |
| Special process records | Available |
What to Include in Your RFQ
To quote quickly and correctly, recommend sending the following:
3D model + 2D drawing (PDF + STEP preferred)
Material grade (e.g., A2 / D2 / H13 / M2) and condition if known
Quantity (prototype vs. repeat order forecast)
Critical characteristics: datums, GD&T, sealing surfaces, fits, runout, flatness
Surface finish, coating, passivation, marking, cleaning, or assembly requirements
Required documents (MTR, FAI, full dimensional, special process certs)
Target delivery date and ship-to country
Supported file formats: STEP/STP, IGES/IGS, X_T/X_B, SLDPRT, SAT; PDF, DWG, DXF.
Max upload per RFQ: 500 MB.
Request a Quote (RFQ)
Send your drawing/model, quantity, material, and required documentation. You will receive:
- A manufacturability review (if needed)
- A clear process route (machining + EDM/grinding + special processes when applicable)
- Quote, lead time options, and inspection/documentation plan
Request a Quote
Tell us about your component requirements and material challenges.